01
Cutting & forming inserts
Inserts for blanking, bending and drawing dies, with wire-cut profiles and a sliding fit in their pocket.
Service 02
Die inserts, punches, dies, shims and hydroforming components. We work hardened tool steel and cut the final geometry after heat treatment — which is where geometry actually survives.
Approach
The most common mistake in tooling is machining final geometry in soft material and sending it out to harden. The part moves, the corner rounds off, and the fit that took hours is lost in the furnace.
We leave critical geometry for last: rough machine, heat treat, then close it out with wire EDM and grinding. The result is an insert that drops into its pocket without stoning, and a corner that stays sharp.
It takes more planning, but it is the difference between tooling that lasts a program and tooling that needs re-fitting every month.
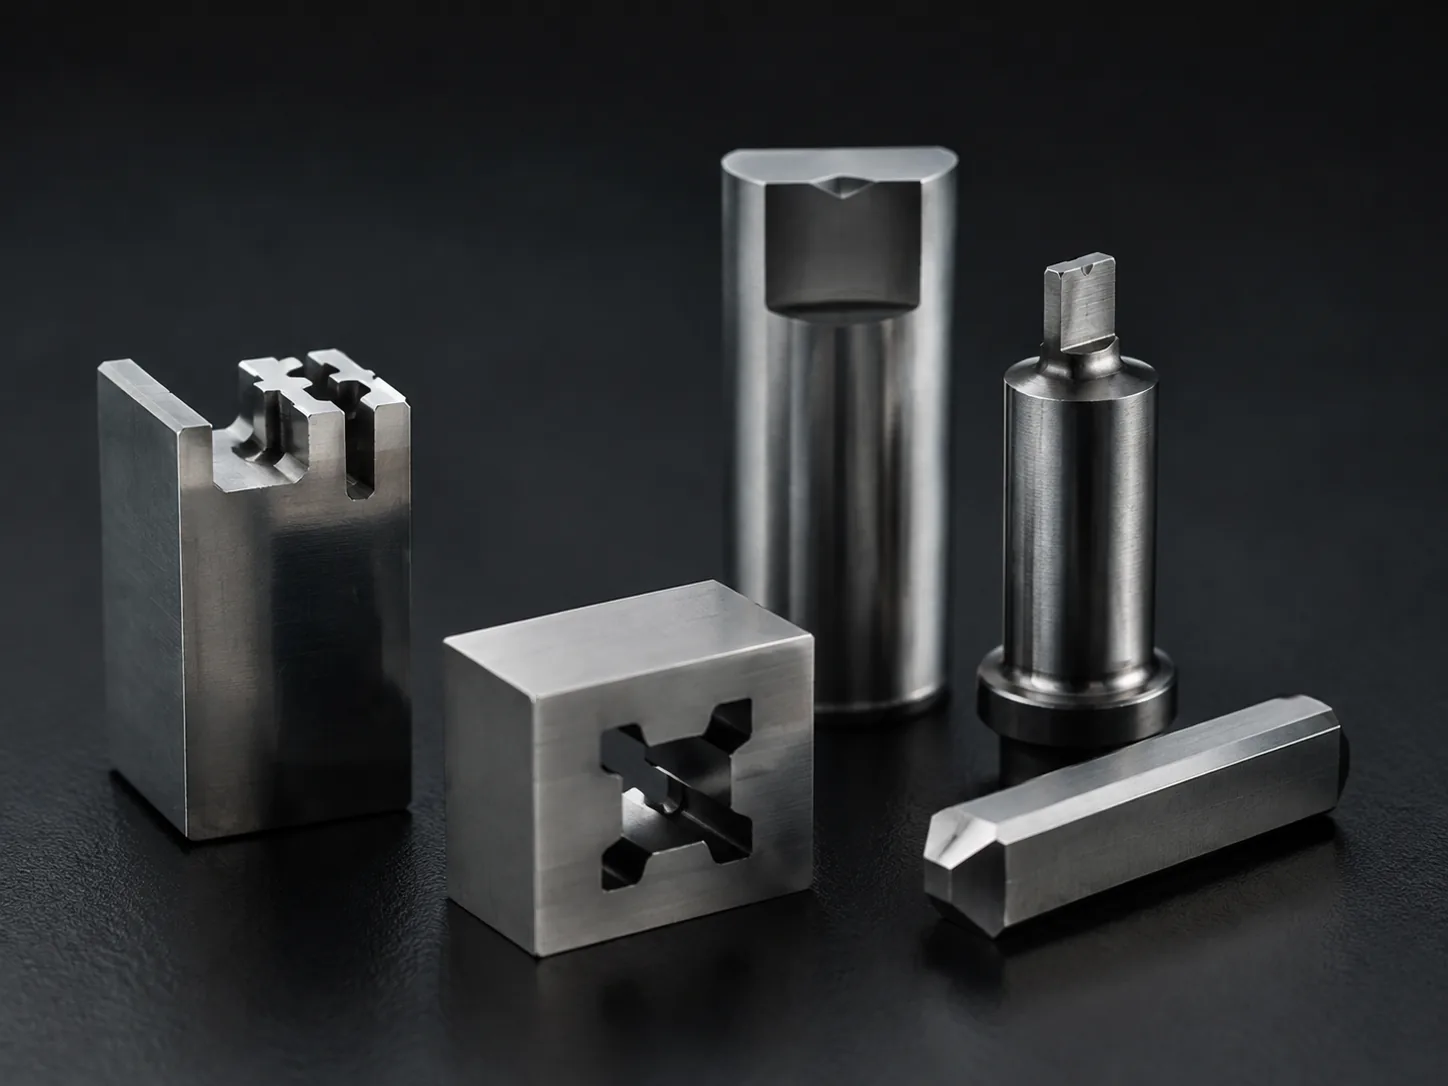 Imagen ilustrativa · Illustrative image
01
Inserts for blanking, bending and drawing dies, with wire-cut profiles and a sliding fit in their pocket.
02
Blanking punches, tube piercing punches and perforating punches, with head, body and point to suit the application.
03
Complete dies and individual replacement components, including guides, bushings and plates.
04
Shims machined to the required thickness to correct heights and clearances, with controlled material and flatness.
05
Inserts, mechanical seals and clamping elements for tube hydroforming tooling.
06
We copy the worn component by scanning or direct measurement and reproduce it, even with no original drawing.
Heat treatment is done by a treater we have worked with for years, and we keep responsibility for the result: if the hardness does not come out as specified, that is our problem, not yours.
Yes. We scan what survived, rebuild the geometry and show you the model before machining so you can confirm. This is routine work for us.
Wire EDM allows tight tolerances and sharp corners in already-hardened material. The committed tolerance is defined per part in the quote based on geometry and material — we do not publish a generic number we cannot then hold.
Yes, and it is a large part of what comes through the door. If a line is stopped, say so in the first message: we re-sequence machine load and give you a real date the same day.
Upload your drawing or 3D model and get a formal quote within 24–48 business hours. If anything is missing from the file, we tell you the same day instead of leaving you waiting.